TL;DR / Key Takeaways
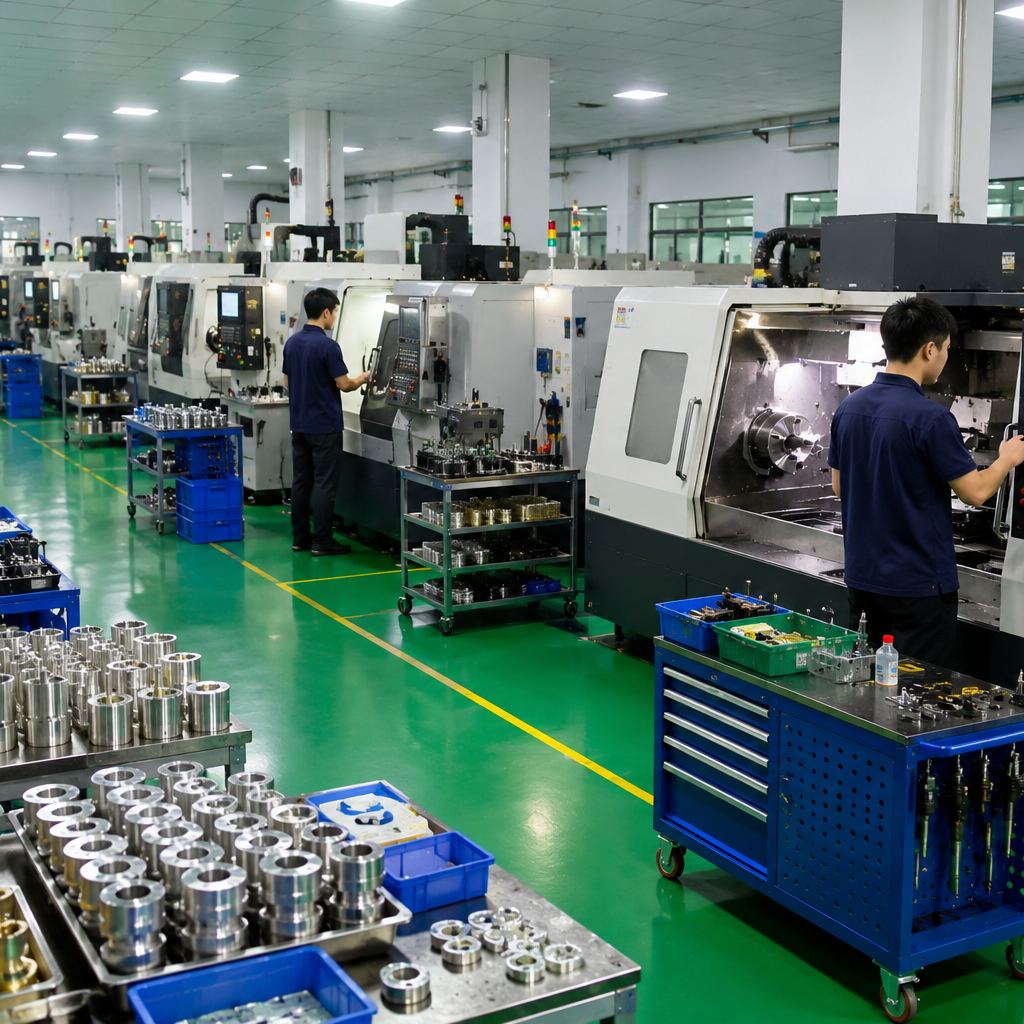
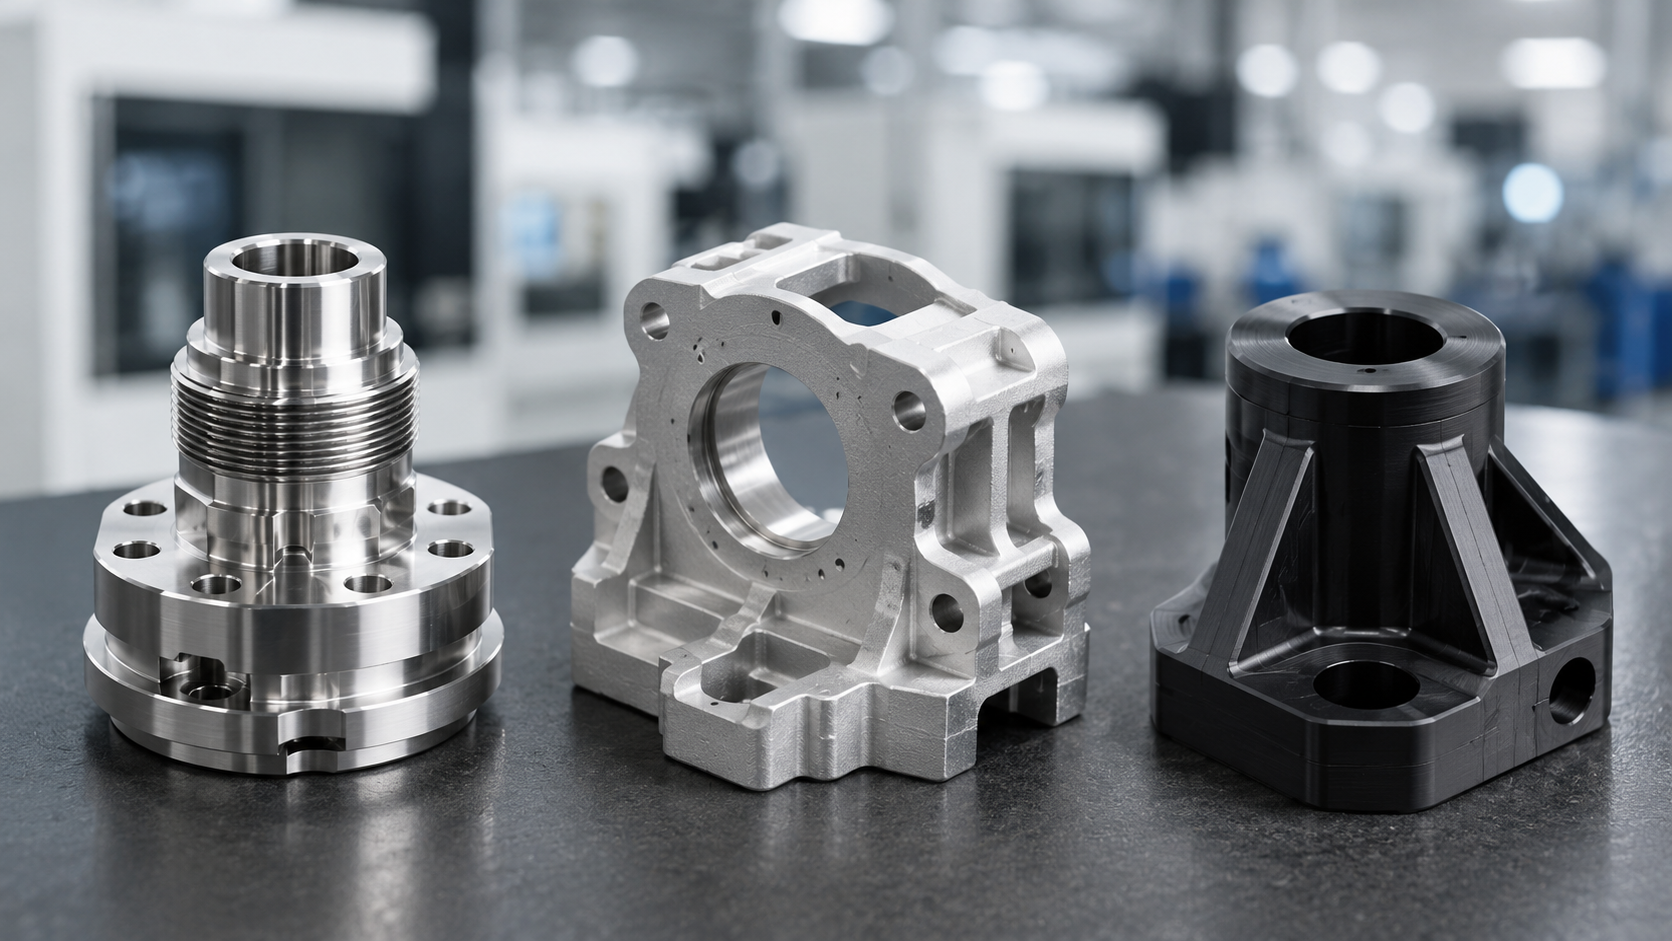
CNC machining (Computer Numerical Control) is a subtractive manufacturing process that utilizes computerized machine tools to remove material from a solid block, yielding highly precise custom parts.
Core Highlights:
Subtractive Method: Unlike 3D printing (which adds layers), CNC carves out the final geometry from raw stock (billets).
Extreme Precision: Consistently achieves tight tolerances (e.g., ±0.005 in or better), making it the gold standard for aerospace, medical, and automotive components.
Driven by Code: Relies on CAD (Computer-Aided Design) models translated into G-code to automate multi-axis movements, ensuring zero human error and exact repeatability for mass production.
The Core Concept: What Does CNC Stand For?
Definition & Brief History
At its core, CNC (Computer Numerical Control) replaces manual operator control with precise, code-driven automation. Instead of a machinist manually turning handwheels or levers, an integrated computer interprets digital instructions to command the exact movement, feed rate, and spindle speed of the cutting tools.
The technology has evolved dramatically since its inception. In the 1950s, early NC (Numerical Control) machines relied on cumbersome punched paper tape to dictate basic, linear movements. Today, modern CNC equipment utilizes advanced CAD/CAM software to execute simultaneous multi-axis continuous paths. This evolution allows manufacturers to produce incredibly complex, organic geometries with zero manual intervention during the active cutting cycle.
CNC Machining vs. 3D Printing
While both are foundational to modern digital manufacturing, they operate on fundamental opposites. CNC machining is a subtractive process (carving material away from a solid block), whereas 3D printing is an additive process (building material up, layer by layer). Understanding when to deploy which method is critical for optimizing both project costs and part performance.
| Dimension | CNC Machining (Subtractive) | 3D Printing (Additive) |
| Material Strength | Excellent. Parts retain the full isotropic mechanical properties of the original solid billet. | Moderate. Parts often exhibit anisotropic properties, making them weaker along the Z-axis (layer lines). |
| Surface Finish | Superior. Capable of achieving extremely smooth finishes (Ra 0.4 µm or better) straight off the machine. | Rougher. Typically leaves visible layer lines, requiring manual post-processing to achieve a smooth finish. |
| Mass Production Scalability | High. Highly cost-effective for medium to high-volume runs once the initial programming and setup are complete. | Low. Slower per-part cycle times make it less economically viable for scaling into mass production. |
| Ideal Use Cases | Load-bearing metal components, tight-tolerance parts, and high-volume precision manufacturing. | Rapid prototyping, highly complex internal lattice structures, and low-volume custom plastics. |
How the CNC Machining Process Works
Step 1: CAD Model & DFM
The manufacturing process begins by creating a precise 2D or 3D digital rendering using Computer-Aided Design (CAD) software. This stage demands a strict Design for Manufacturability (DFM) review to ensure the part’s geometry avoids impossible tool paths, excessively deep cavities, or unnecessary features that drive up machining time and costs.
Step 2: CAM & G-Code/M-Code
Once the design is finalized, Computer-Aided Manufacturing (CAM) software translates the CAD model into machine-readable logic. It generates G-code (geometric code) to dictate exact tool movements, paths, and feed rates, alongside M-code (miscellaneous code) to control auxiliary machine functions like coolant activation and automated tool changes.
Step 3: Workholding & Setup
Before cutting initiates, the operator secures the raw material block using rigid workholding devices (vises, chucks, or custom fixtures) to eliminate vibration. Accurately defining the “work offset” (the absolute zero reference point) is vital. The machine must know exactly where the physical stock sits relative to the digital coordinates to maintain tight tolerances.
Step 4: Execution & Precision Control
With the setup verified, the CNC machine executes the subtractive operations autonomously. Advanced machining centers rely on closed-loop servo systems to constantly monitor and adjust tool positioning. This real-time feedback ensures dimensional accuracy and micron-level precision from the first roughing pass to the final finishing cut.
Common Types of CNC Machines & Operations
CNC Milling
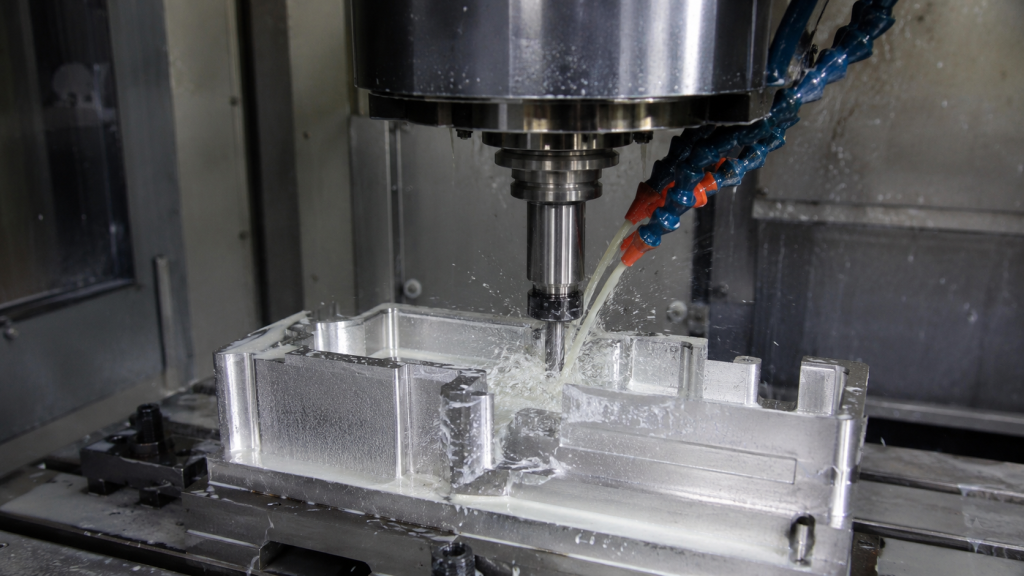
CNC milling utilizes rotating multi-point cutting tools to remove material from a secured workpiece. While standard 3-axis mills (operating along the X, Y, and Z linear axes) are highly efficient for flat geometries and straightforward profiles, advanced 4-axis and simultaneous 5-axis machining centers introduce rotational movement. This allows the machine to approach the workpiece from virtually any angle, enabling the fabrication of highly complex, undercut, and multi-sided geometries in a single setup—drastically improving alignment precision and reducing lead times.
CNC Turning & Swiss-Type Machining
In CNC turning, the workpiece rotates at high speeds in a chuck while a stationary single-point cutting tool shapes it into precise cylindrical profiles. For extreme precision on small parts, Swiss-type automatic lathes (such as the industry-leading Citizen brand) offer an absolute advantage. Unlike conventional lathes, Swiss machines feed the raw bar stock through a guide bushing, supporting the material mere millimeters from the cutting tool. This completely eliminates tool deflection and vibration, making Citizen Swiss-type machining the gold standard for producing long, slender, and micro-complex components with exceptionally tight tolerances.
CNC Drilling & Secondary Operations
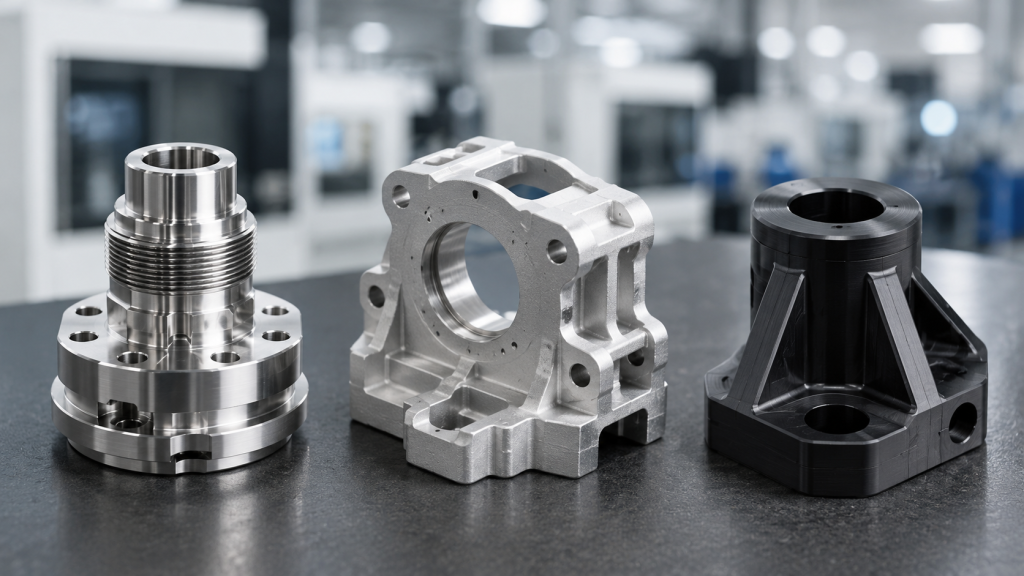
While milling and turning define the primary geometry, comprehensive manufacturing relies on precise secondary operations. CNC drilling employs rotating bits to create cylindrical holes, utilizing specialized “peck-drilling” cycles for deep-hole applications to efficiently clear metal chips and prevent heat buildup. Tapping is then used to cut precise internal threads for fasteners. Modern, multi-tasking CNC centers can seamlessly integrate these operations—alongside reaming, boring, and surface finishing—into the primary machining cycle to guarantee perfect concentricity and flawless final assembl
Key Cost Drivers in CNC Machining
Material Selection
The raw material chosen establishes the baseline cost of any project. Materials with a high machinability rating (such as aluminum alloys or brass) cut quickly and cleanly, minimizing active machine time. Conversely, tough alloys like titanium, Inconel, or 17-4PH stainless steel have poor machinability. They require slower spindle speeds and extended cycle times, and they cause rapid tool wear. The need for frequent replacement of specialized carbide cutting tools will directly inflate the per-part cost.
Part Complexity & Tolerances
Complex part geometries featuring deep cavities, thin walls, or undercuts require advanced 5-axis machines, specialized tooling, and prolonged programming times. Furthermore, demanding extremely tight tolerances (e.g., ±0.001 in or tighter) significantly increases manufacturing costs. Achieving such precision demands meticulous machine calibration, slower feed rates to prevent material deflection, and highly stringent post-machining quality inspections. Relaxing non-critical tolerances during the DFM phase is the most effective way to optimize costs.
Production Volume
CNC machining is characterized by high initial setup costs—encompassing CAD/CAM programming, tool preparation, and physical machine calibration. In low-volume prototyping, this fixed cost is absorbed by only one or a few parts, resulting in a high unit price. However, as production scales into medium and high-volume runs, these fixed setup expenses are amortized (spread out) across thousands of units. Consequently, the price per part drops dramatically, making CNC a highly economical solution for scalable mass production.
High-Performance Materials for CNC Machining
Stainless Steel & Specialty Alloys
While standard austenitic grades like 304 and 316 stainless steel are heavily relied upon for their excellent corrosion resistance, they are prone to work-hardening and require careful thermal management during cutting. Moving up the performance tier, 17-4PH (precipitation hardening) stainless steel presents a formidable challenge. Achieving tight tolerances on this high-strength, tough alloy requires ultra-rigid machine setups, specialized coated carbide tooling, and high-pressure coolant strategies to prevent rapid tool degradation and maintain a flawless surface finish.
Aluminum Alloys
Aluminum is universally favored for its exceptional machinability, allowing for aggressive feed rates and minimal tool wear. Beyond machining from raw solid billets, CNC centers play a critical role in the secondary machining of die-cast aluminum alloys, specifically A356.2 and ADC12. Because die casting economically produces a near-net shape, CNC operations are highly targeted—used exclusively to finish critical mating surfaces, bore precise bearing journals, and tap tight-tolerance threaded holes, perfectly blending high-volume casting speed with micron-level accuracy.
Engineering Plastics
CNC machining is equally effective for technical polymers requiring precise structural integrity. ABS provides an economical, impact-resistant solution for functional prototypes. POM (Delrin) is an industry favorite due to its inherent low friction, high stiffness, and superb dimensional stability, making it ideal for precision gears and insulating bushings. At the apex of polymer performance, PEEK delivers extreme thermal and chemical resistance, frequently replacing heavy metal components in demanding aerospace and biocompatible medical device applications.
Real-World Industrial Applications
High-Performance Motors
The demand for high-RPM brushless motors requires absolute concentricity and dynamic balance. CNC machining is the only subtractive method capable of consistently producing these critical internal components. From turning ultra-straight precision shafts and milling intricate stator cores to cutting highly durable locating collars, advanced CNC centers ensure these motor assemblies operate flawlessly under extreme speeds and thermal stress without vibration.
Automotive Components
The modern automotive sector—especially the rapidly expanding Electric Vehicle (EV) market—relies heavily on CNC machining for safety-critical assemblies. Components like precision actuators, custom fluid control valves, and complex sensor housings must be manufactured to exact specifications. Facilities operating under strict IATF 16949 quality management systems utilize automated CNC technology to guarantee zero-defect production, ensuring every component meets the industry’s rigorous reliability standards.
Medical & Aerospace Precision Parts
In industries where failure is not an option, CNC machining delivers the ultimate in material integrity and dimensional accuracy. For the medical sector, multi-axis and Swiss-type machines carve intricate, biocompatible surgical instruments and implants from solid titanium or PEEK. Similarly, the aerospace industry depends on CNC machining to produce high-strength, lightweight structural elements—such as landing gear fittings and engine housings—where maintaining strict weight-to-strength ratios is paramount.
How to Choose a Reliable CNC Machining Partner
Global Quality Certifications
Sourcing precision parts globally carries inherent risks, making robust quality management systems non-negotiable. A reliable partner proves their capability through internationally recognized frameworks. Facilities operating under ISO 9001 and ISO 14001 demonstrate a strict commitment to consistent quality control and environmental responsibility. More importantly, securing a supplier with the stringent IATF 16949 certification ensures they utilize advanced defect-prevention protocols and rigorous traceability, eliminating procurement risks right from the raw material stage.
Integrated Supply Chain Capabilities
Smart procurement managers understand that top-tier suppliers offer more than just a floor full of CNC machines. Complex projects frequently require a blend of manufacturing methods. Partnering with a comprehensive manufacturer like Dongguan Yongyuan Hardware Technology Co., Ltd. provides a true “One-Stop” solution. By seamlessly integrating high-pressure die casting, progressive die stamping, and precision CNC secondary machining under one roof, you eliminate the logistical nightmare of managing multiple vendors. This consolidation drastically slashes lead times, ensures uniform quality control, and significantly reduces cross-border communication costs.
Frequently Asked Questions (FAQs)
What is the difference between CNC milling and turning?
The fundamental difference lies in the motion of the machine. In CNC milling, a multi-point cutting tool rotates and moves across a secured, stationary workpiece, making it ideal for flat, irregular, or prismatic shapes. In CNC turning (lathes), the raw material itself spins at high speeds against a stationary, single-point cutting tool, making it the superior method for crafting precise cylindrical components like shafts and bushings.
How much does CNC machining cost?
There is no universal price tag. Machining costs are determined by three main factors: raw material (machinability and market price), part complexity (which dictates programming time and tool wear), and production volume. Because CNC involves initial fixed setup costs, single prototypes are relatively expensive. However, as production volume increases, these setup costs are distributed, dramatically lowering the price per part.
Is CNC machining better than 3D printing?
Neither is universally “better”—they serve completely different manufacturing needs. CNC machining is the superior choice for end-use parts that require full structural integrity (isotropic strength), tight mechanical tolerances, and specific metal properties. 3D printing (additive manufacturing) excels at rapid prototyping and building complex internal geometries (like lattice structures) that traditional cutting tools physically cannot reach.